


Production Technology
- Home
- Technology and Quality
- Production Technology
Production Technology
Engraving
After a customer places an order, the mold department first creates a 3D model of the product and mold based on the customer's drawings. Then, using CNC machining, electrical discharge machining, and etching techniques, they fabricate the mold core. Depending on product requirements, a special mold base may need to be made. Once the mold is complete, trial production die casting is conducted, and the mold is fine-tuned. After confirming the sample with the customer, mass production can begin.
 CNC die making | Electrical Discharge Machining |
| Etching patterns | Mold frame and mold core |
| 3D design | 3D design |
Die casting
The die-casting department first installs the product mold core and mold frame on the die-casting machine, and adjusts the furnace temperature and injection pressure. If necessary, cooling water channels also need to be set up to maintain the dimensional stability of the finished product and minimize deformation. After the setup is complete, the quality of the trial-pressed black blank is confirmed, and the die-casting automation values are set before mass production begins. The semi-finished black blank must be separated from the surrounding material channels to become an individual product black blank.
| Automated die casting | Cooling water circuit design |
Grinding
Injection-molded products have parting lines, and metal products are no exception. The mold joints cause different burrs on the die-cast blanks, which need to be removed manually or semi-automatically using different tools. When forming black blanks, temperature differences and micro-bubbles also cause rough surfaces that are not easily visible to the naked eye. After polishing, the gloss and surface smoothness of electroplating can be enhanced, and even a mirror effect can be achieved.
| Automatic grinding and polishing | Magnetic grinding |
Plating
The electroplating process involves hot chamber die casting of zinc alloy, followed by deburring and polishing, cleaning the substrate to make its surface smooth; then plating with copper cyanide, copper pyrophosphate, copper sulfate, etc. to form a copper base, followed by nickel plating, and finally plating with other colors. After completion, a sealing oil is applied.
| Color electrophoresis | Color electrophoresis |
| Two-color electroplating | Multicolor electroplating |
Coloring
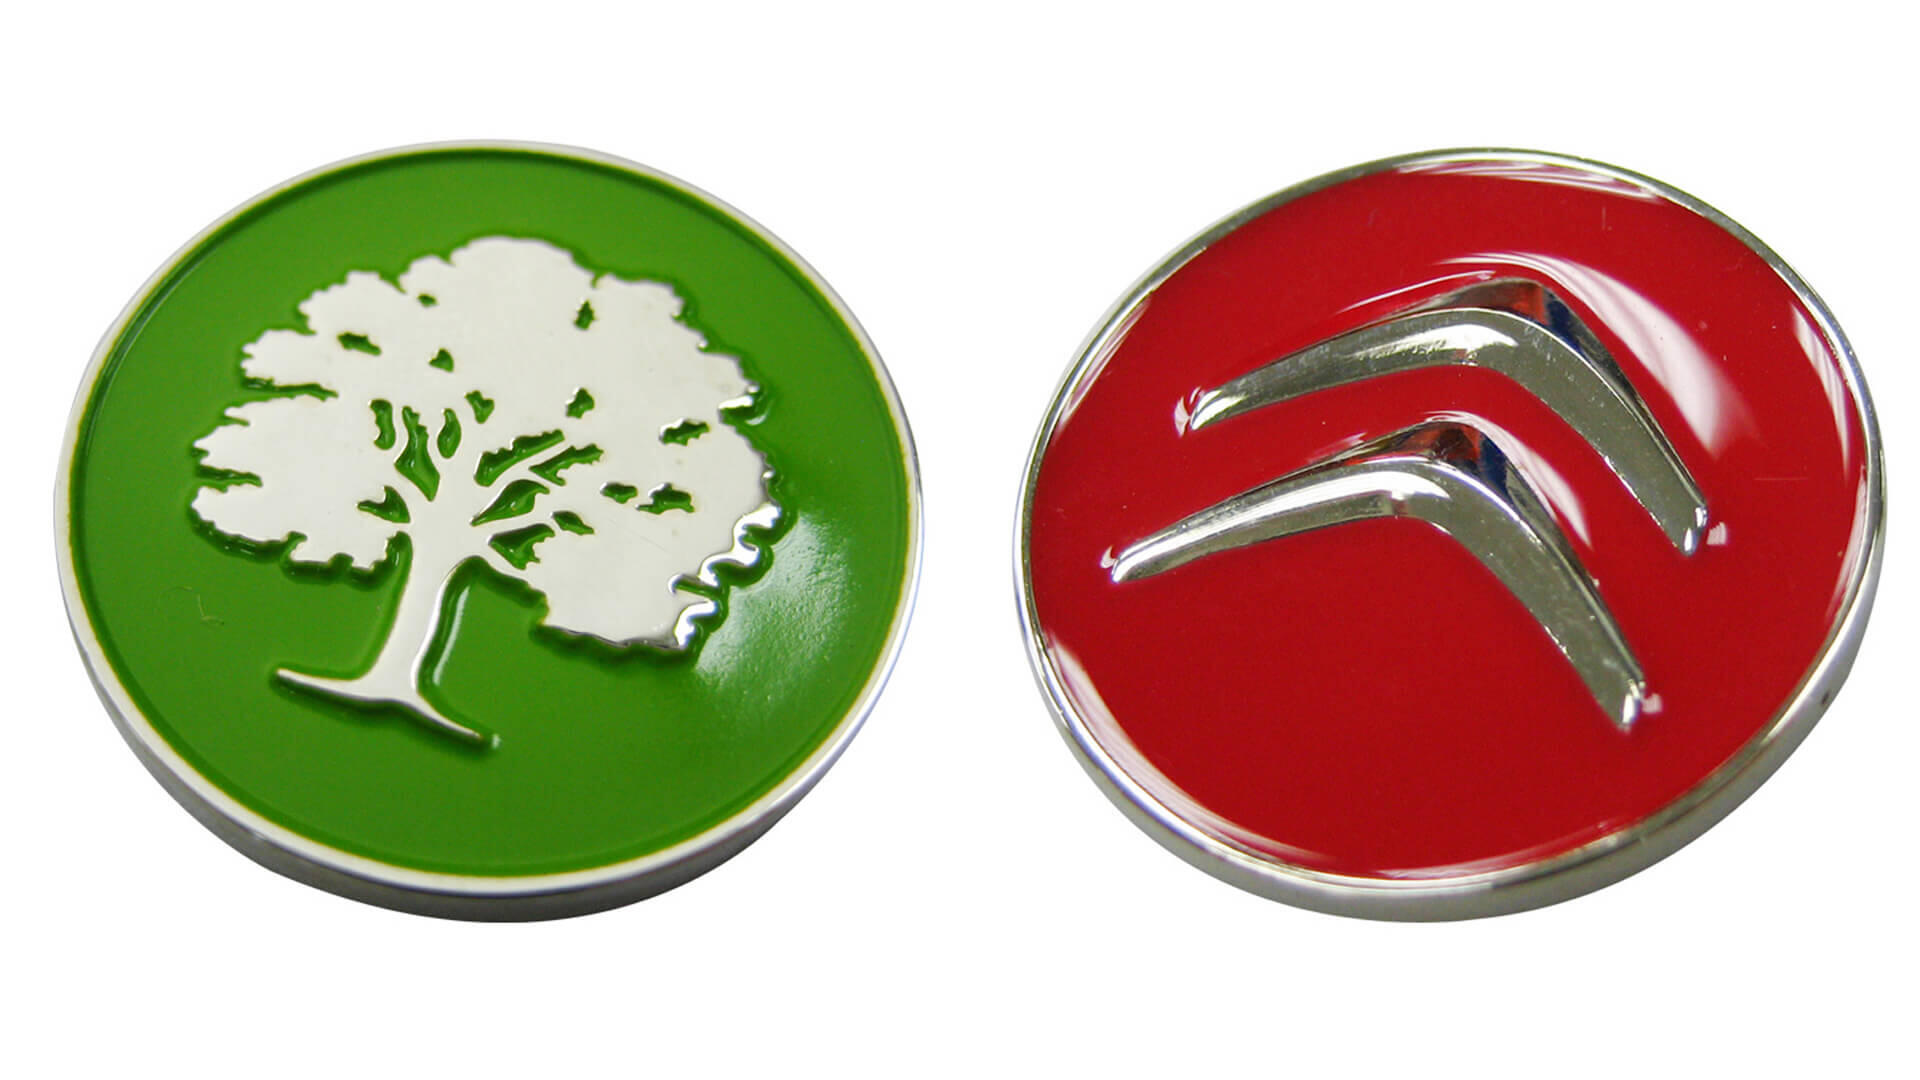
After polishing and electroplating, colorants can be added to the recessed and enclosed areas of the semi-finished product to color it.
Colorants can be categorized into three main types: baked enamel, colored polychrome, and imitation enamel.
Baked paint has a matte finish; colored paint, after curing, has vibrant colors and a glossy finish.
Imitation enamel requires adding colorant after polishing the black blank of the product, and then polishing it again after it has cured until the metal lines that distinguish the color blocks are revealed, and finally electroplating.
Therefore, fake enamel products show subtle polishing marks, and the metal lines and the colored areas are at the same height.
 Soft Enamel / Colorful Epoxy | UV digital printing |
| Soft cloisonne | Spray paint |
Package
In addition to protecting goods during transportation, packaging is also seen as the face of the product, thereby promoting sales.
With decades of product experience, we understand the characteristics of various packaging materials. We have suppliers of various packaging materials to help you achieve better product matching results.
| Automatic packaging |